One connected production process
Material batching, mixing, conveying, moulding and pallet handling work together on the QT5-15 line, followed by curing.
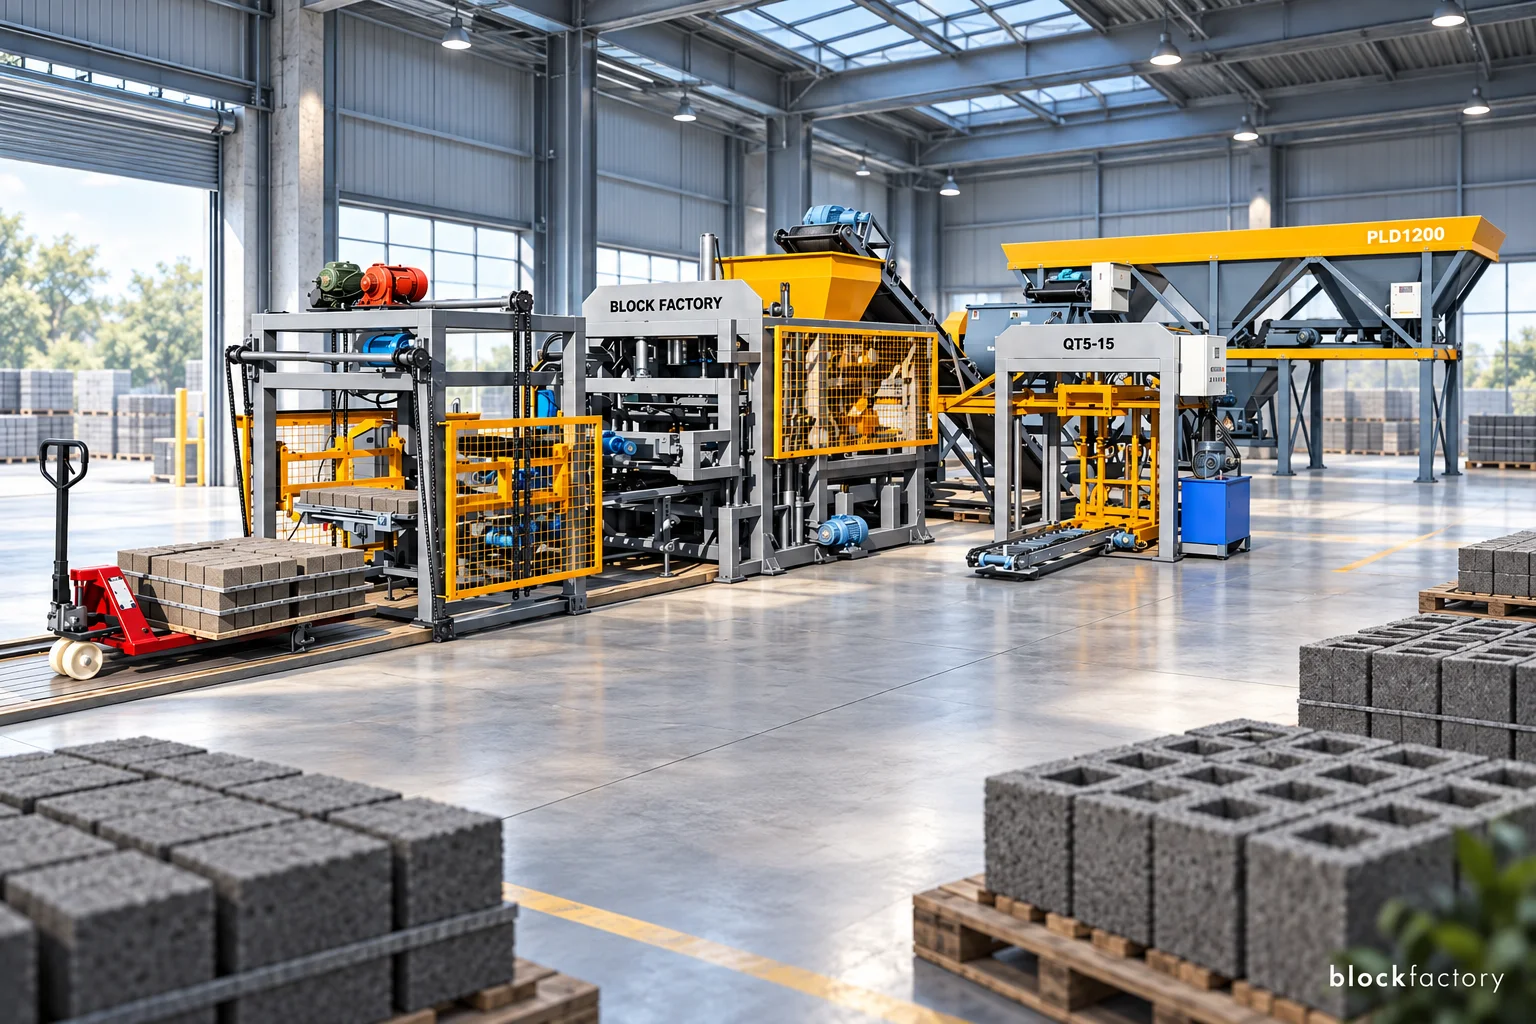
Illustrative production-line visualization
Stages
From batching to stacking
Six stages on the line. Curing follows stacking, once loaded pallets leave the stacker.
Batching
The PLD1200 three-bin batching station prepares aggregate for transfer.
Mixing
An 8 m conveyor feeds the batched material to the JS500 mixer.
Feeding
Mixed material travels by conveyor to the main machine hopper.
Moulding
The QT5-15 combines hydraulic mould movement with vibration.
Transfer
The pallet feeder and block conveyor move formed products out of the moulding area.
Stacking
The stacker handles loaded pallets before the products go to curing.
Equipment
The equipment behind each stage
As described in the QT5-15 installation and operation manual, with photographs from the manual. Final scope depends on the confirmed order.
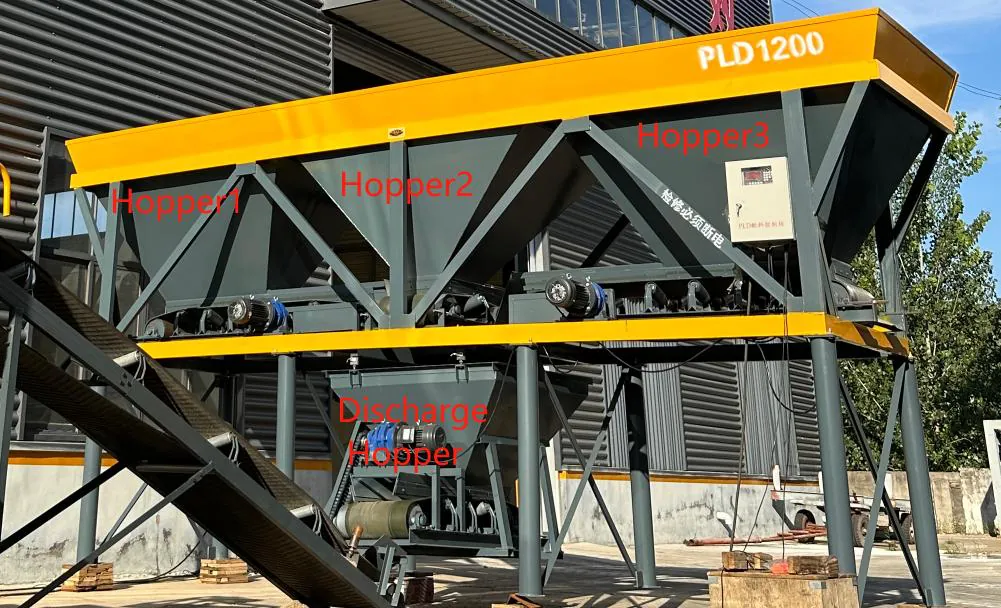
PLD1200 batching station: three bins above the discharge hopper. Source: QT5-15 installation and operation manual, p. 9.
PLD1200 batching station
Three aggregate bins with a weighing hopper on load cells, discharging onto the mixer feed conveyor.
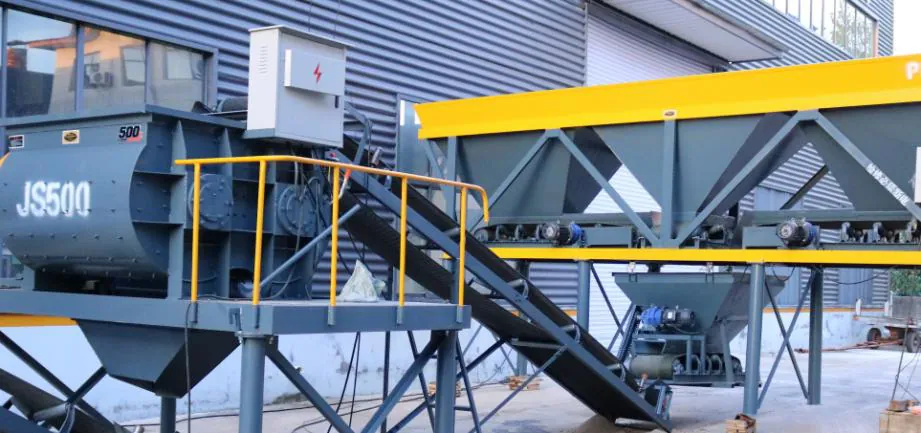
Belt conveyor rising from the batching station to the JS500 mixer. Source: QT5-15 installation and operation manual, p. 10.
Batching-to-mixer conveyor
8 m belt conveyor receiving material from the PLD1200 discharge hopper.
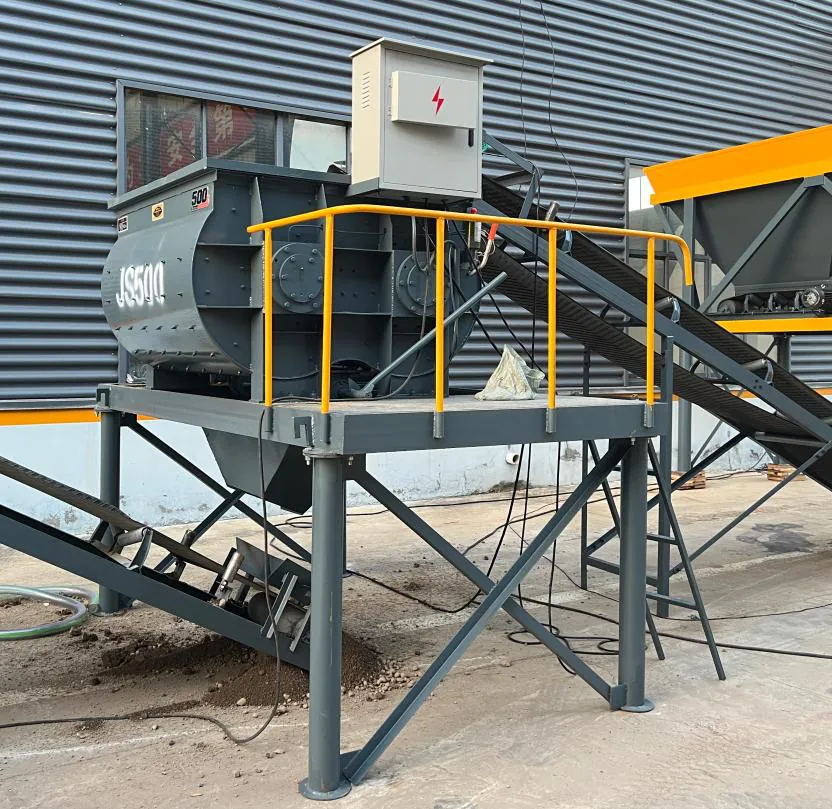
JS500 mixer with its control box and worker guardrail. Source: QT5-15 installation and operation manual, p. 11.
JS500 mixer
Mixes the batched material before it is conveyed to the main machine.
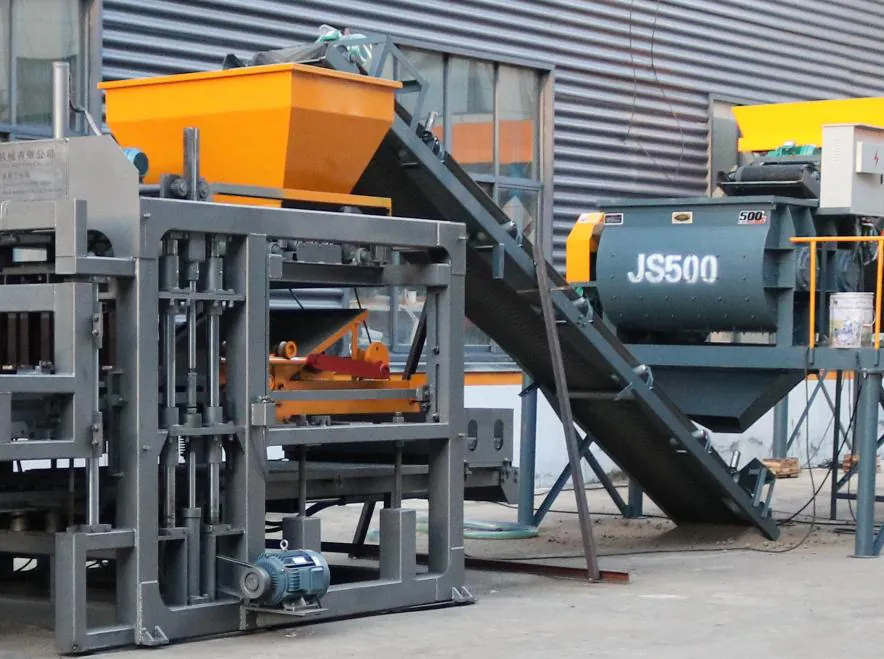
Feeding conveyor from the JS500 mixer to the QT5-15 hopper. Source: QT5-15 installation and operation manual, p. 13.
Main machine feeding conveyor
Inclined belt conveyor carrying mixed material to the QT5-15 hopper.
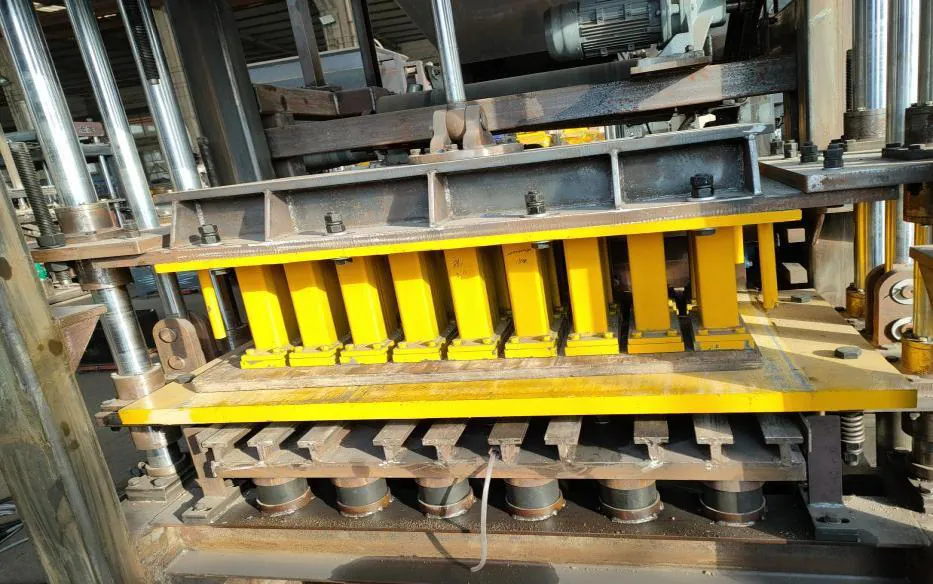
Upper mould pressure head above the lower mould. Source: QT5-15 installation and operation manual, p. 23.
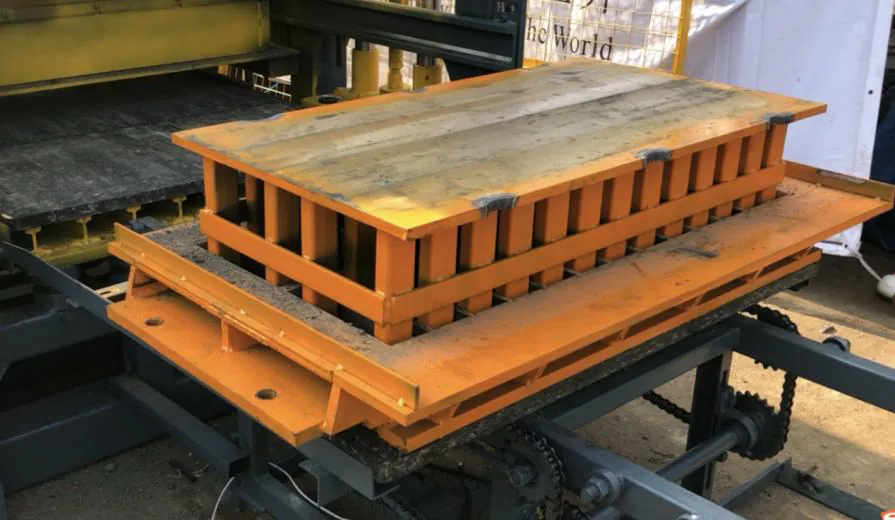
Block mould on a pallet during a mould change. Source: QT5-15 installation and operation manual, p. 25.
QT5-15 main machine
Hydraulic upper and lower mould movement, material feeding box and vibration platform.
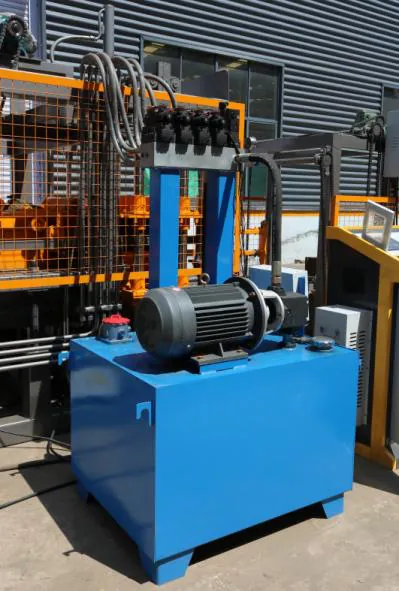
Hydraulic station: oil tank, pump motor and valve block. Source: QT5-15 installation and operation manual, p. 14.
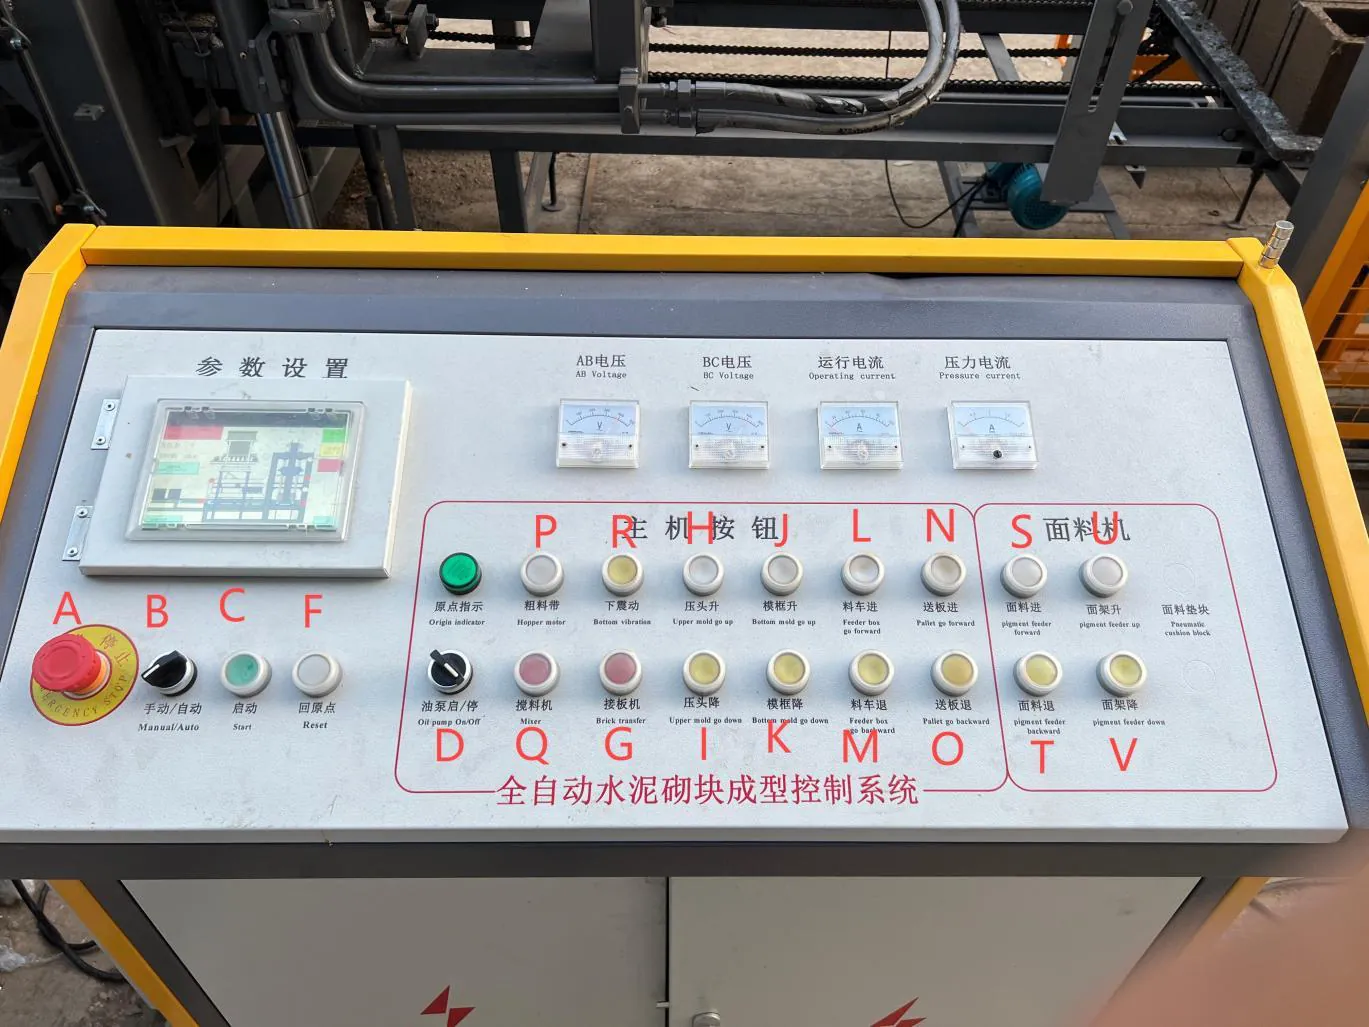
PLC control panel. Source: QT5-15 installation and operation manual, p. 4.
Hydraulic station and PLC control cabinet
Hydraulic pump, oil tank with water cooling, and the control panel for automatic and manual operation.
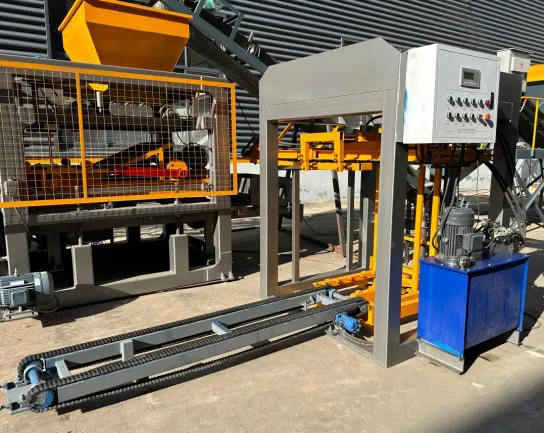
Pallet feeder in front of the main machine. Source: QT5-15 installation and operation manual, p. 17.
Pallet feeder and block conveyor
Feeds empty pallets into the moulding area and moves formed products out.
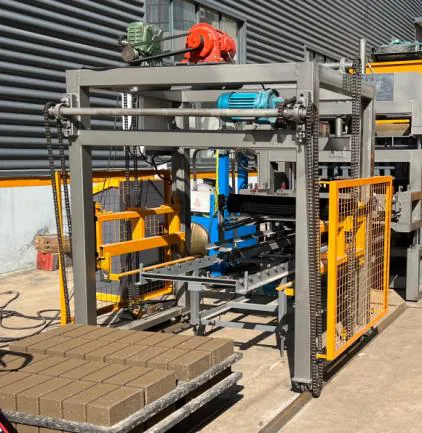
Automatic stacker with a pallet of formed blocks. Source: QT5-15 installation and operation manual, p. 19.
Stacker
Automatic stacker running on rails at the end of the block conveyor.
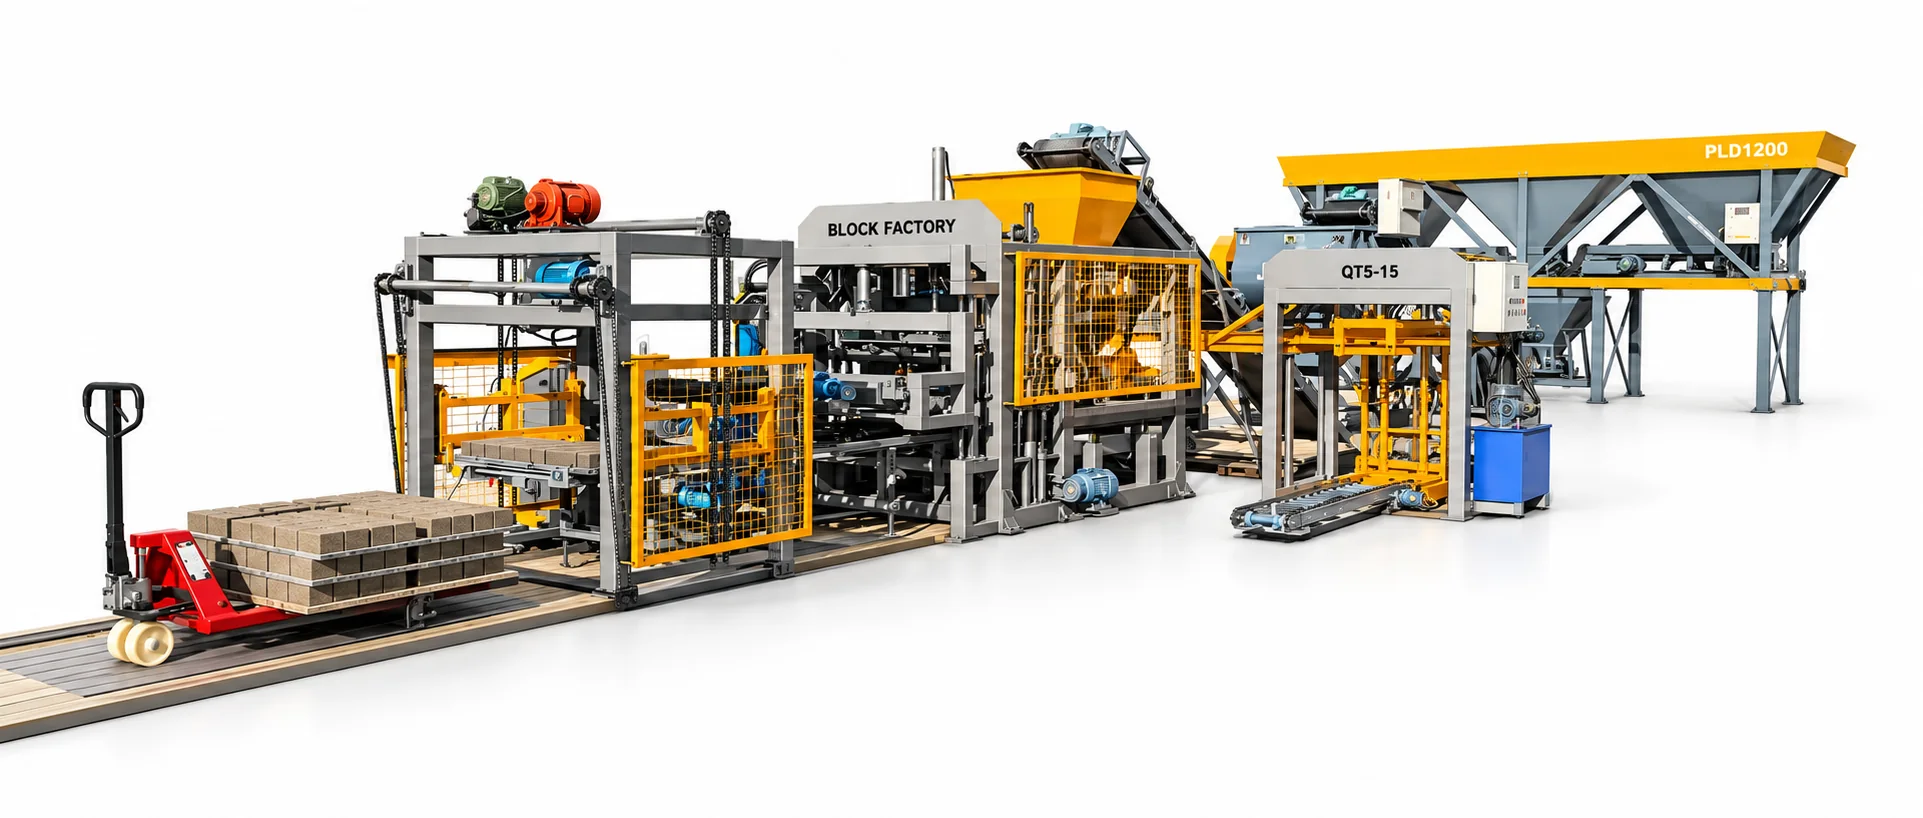
Complete QT5-15 line overview, from the company profile.
Planning the line
- The whole production line covers an area of approximately 35 × 21 m.
- The workshop needs a clear height of more than 6 m.
- Electrical supply: 380 V, 50 Hz, three-phase.
- Site preparation, foundations and services must follow approved project drawings.
Configuration, moulds, product dimensions and achievable output must be confirmed for your project before ordering. Line arrangement and supplied equipment depend on the confirmed order.